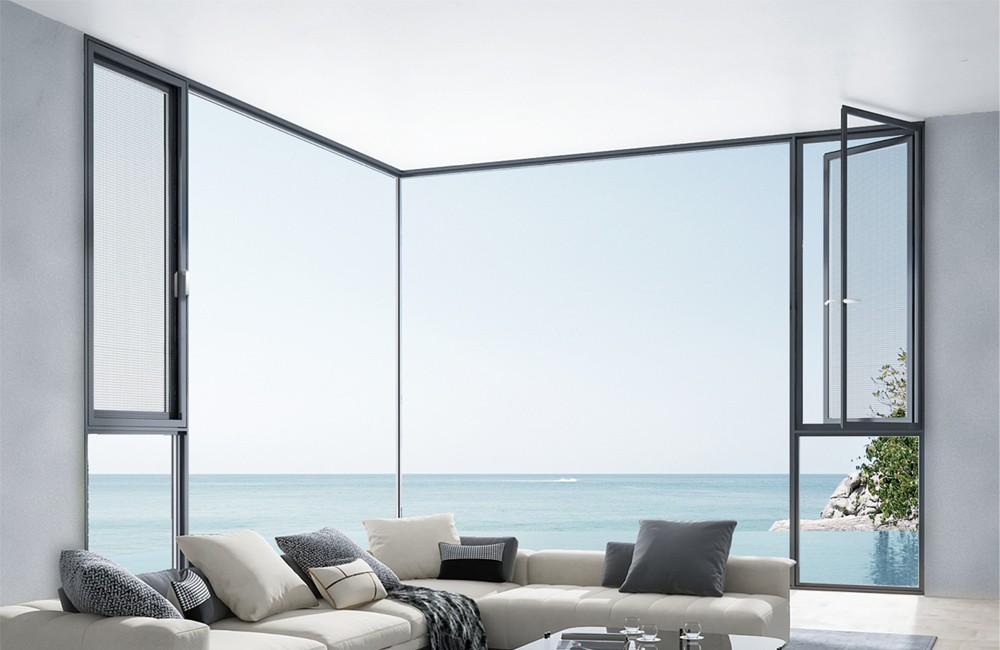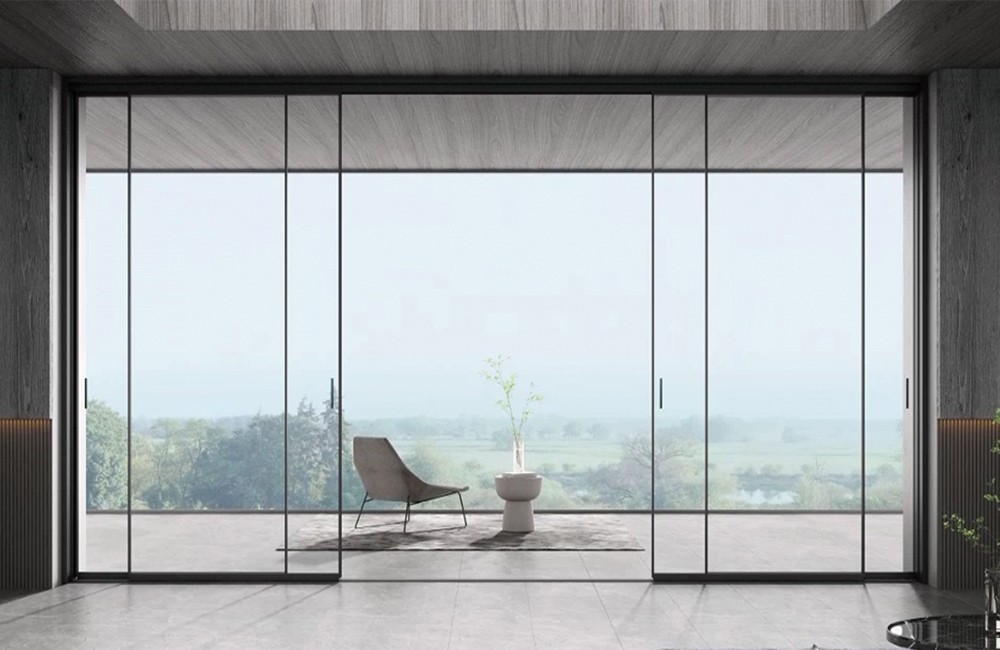
A sliding door is mostly two things: a very large piece of glass, and a set of decisions about what holds it. The word seamless belongs entirely to the second group, and it is one of the most reliably misunderstood adjectives in this industry. It does not describe a performance. It describes the absence of something, and the thing being removed is not the same thing in every factory.
This article is about the SL182 thermal break sliding door, and specifically about the phrase seamless frame. Our own published wording for this series is seamless frame design, pressure-line-free, smooth surface. The argument here is that the pressure line is not decoration: it is simultaneously a fastener, an access panel and a finished edge, and removing it moves a cost from the first day of the project to the day the glass has to come out. That trade can be a good one. It should be made deliberately, and in most enquiries it is not made at all.
Before anything else, the word has to be split. In aluminium doors and windows it is used for at least three unrelated decisions. They are bought by different people, at different moments, and only one of them is reversible after the order is placed.
| What the speaker means | What is physically removed | Who decides it | When it stops being changeable | What it costs you later |
|---|---|---|---|---|
| No glazing bead, no pressure line holding the glass into the sash | The removable strip around the glass perimeter | The system designer, years before your project | At extrusion tooling, so effectively never | Glass replacement stops being a one-visit job with a knife |
| Seamless welded corners, no visible joint where two profiles meet | The mitre line, by welding, grinding and then coating | The fabricator's process choice | When the frame is assembled | A disputed strength question, discussed below |
| Flush threshold, no visible step or rail in the floor | The upstand that keeps water out | The structural engineer and the waterproofing designer, not the door supplier | When the slab is poured | The drainage path becomes a building problem, not a product problem |
This series sits in the first row. We publish pressure-line-free in the feature list. We publish nothing about welded corners for this series, and nothing that would let you infer the third row. The three rows get conflated constantly in enquiries, and the confusion is expensive, because a buyer who asks for the third row and is sold the first row will not discover the difference until the first heavy rain.
The series is published in two sash widths under the same frame designation. Both are thermal break sliding doors, both are offered in two-track and three-track versions, and the published numbers below are the entire published specification.
| Published item | SL126/182(96) | SL126/182(75) | What that number actually measures |
|---|---|---|---|
| Profile grade | 6060-T66 | 6060-T66 | The alloy and temper. Identical across our range, so it does not distinguish this door from any other we make |
| Profile thickness | 2.0 mm, locally reinforced to 3.0 mm | 2.0 mm, locally reinforced to 3.0 mm | Wall thickness of the extrusion. The reinforcement is local, so ask where |
| Frame wall width | Two track 126 mm, three track 182 mm | Two track 126 mm, three track 182 mm | How deep the frame goes into the wall. Not a sightline and not a wall thickness |
| Glass sash thickness | 55 mm | 55 mm | The stack-up of the sash. It is not the glass pocket, which is a different measurement taken off a section drawing |
| Sash width | 96 mm | 75 mm | The visible face of the moving panel. This is what your eye lands on |
| Frame width | 36 mm | 36 mm | The visible outer member. This is the member the word seamless is attached to in our literature |
| Track height | High 43 mm, low 8 mm | High 43 mm, low 8 mm | Two different rails. The lower figure is the flush option, the higher one is the water defence |
| Opening method | Sliding or lift-sliding | Sliding or lift-sliding | Two different gear sets, and they do not weigh the same or cost the same |
| Published max single sash | 2500 mm wide by 3000 mm high | Not separately published | A size that is always conditional on a glass build-up that is not printed next to it |
| Screen | 80# black or grey stainless mesh | 80# black or grey stainless mesh | A second panel in the same opening, with its own movement and its own cleaning side |
SL182 is not a model code in the automotive sense. The 182 is the three-track frame wall width: how deep the frame sits into the wall. The same series in two-track form is 126 mm deep. So the number that names the product is a dimension that is completely invisible once the door is installed, and it is not the dimension that appears in the marketing photography.
This matters twice. First, frame depth is a property of the series, not a function of track count in any reliable way across a catalogue: a four-track frame in another of our series is shallower than this three-track one. Second, the depth is what your wall has to swallow. If the wall is built and the reveal is set before anybody reads the 182, the conversation becomes a remediation conversation.
For a wider look at how our sliding range is specified and where it has been used, see 60x80 sliding door.
Most people picture a bead as a short line in a corner. It is not. It runs the whole way round the glass, on every glazed panel, four mitred corners per panel. Once you measure it as a length, the decision to delete it changes shape.
Our arithmetic, using the published maximum single sash of 2500 mm by 3000 mm and subtracting the published sash width on all four sides to estimate the glass pocket. Assumptions are stated because they are yours to change: the sash width is applied on all four sides, and the bead run is taken as the glass perimeter.
| Variant | Sash width | Estimated glass pocket (our arithmetic) | Bead run per panel | Mitred corners per panel |
|---|---|---|---|---|
| SL126/182(96) | 96 mm | 2308 by 2808 mm, about 6.5 square metres | About 10.2 metres | 4 |
| SL126/182(75) | 75 mm | 2350 by 2850 mm, about 6.7 square metres | About 10.4 metres | 4 |
| Three panels on a three-track frame | As above | Roughly three times | About 30 metres | 12 |
Two things fall out of that. The first is scale: this is not a detail, it is thirty metres of one joint on a single three-panel door, and every metre of it is a place where air, water and dirt have an opinion.
The second is the counter-intuitive one. The slimmer sash has the longer seam, by about 200 mm on the same opening, because there is more glass to go around. Anyone buying the narrow-sightline version to reduce visual clutter is buying slightly more of the line that the seamless claim removes. That is not an argument against it. It is an argument for understanding what the claim is about.
A glazing bead, called a pressure line in Chinese practice, a glass retainer strip or glazing bead in English, is described in the trade literature as three things at once. It is worth separating them, because seamless deletes all three simultaneously and only one of them is about appearance.
| Role | What it is actually doing | What happens when it is designed out |
|---|---|---|
| Mechanical fastener | Compresses the glass against the rebate gasket, holds it under wind load and vibration, and absorbs the tolerance between glass thickness and pocket depth | Something else has to carry the retention: an adhesive bond, or a sash assembled around the glass |
| Access panel | Lets a glazier remove and refit the pane with hand tools, from one side, without disturbing the frame or the finishes | Glass replacement becomes a different trade with a different tool set and, in the bonded case, a cure schedule |
| Finisher | Hides the setting blocks, the spacer edge and the cut edge of the glass, and frames the visible glass line | The glass edge and the shadow gap become part of the elevation, and the cut edge quality becomes visible |
The second row is the one that never appears in a brochure. A bead is the reason a broken pane is a maintenance call rather than a construction project. There is a fourth consequence too, and it cuts in the opposite direction: externally beaded units can be de-glazed from outside, which is why internal beading is treated as the preferred arrangement for accessible elevations. A unit with no bead to lever has no bead to lever from either side.
Once the bead is gone, the glass is still being held by something. In practice there are three families, and they have almost nothing in common on the day the glass fails.
| Retention method | How the glass comes out | Who can do it | The real cost centre |
|---|---|---|---|
| Removable bead, internal or external | Pry the strip from the middle outward, lift the unit out, set the new one on setting blocks, refit | A glazier with hand tools | Glass cost and labour hours, day one to day one |
| Sash assembled around the glass, corners closed after glazing | The sash corner joint has to be opened. The panel is dismantled, not opened | A fabricator, usually back at a workshop | The sash itself is consumed. In practice the whole panel is often replaced |
| Structural adhesive bond to the sash or to a carrier frame | Cut the pane out, leave a controlled thickness of cured adhesive on the metal, clean to the sealant maker's procedure, re-bond, clamp, wait for cure | Trained personnel following the adhesive manufacturer's written procedure | Days of cure, access equipment, and a bond that must not be loaded until it has cured |
For this series we publish seamless frame design, pressure-line-free, smooth surface, and we also publish true full seal, continuous four-side sealing strips plus sealant between top track and frame. We do not publish which of the three families above replaces the pressure line. That is the single most valuable question in this whole article, and it is not answered anywhere in our public material. Please ask it in writing.
If the answer is a structural bond, the cost of the seamless line is measured in days, not millimetres. A sealant manufacturer's published structural glazing guideline sets out the re-bonding sequence in detail: cut the broken pane out leaving roughly one to two millimetres of adhesive on the metal frame and never scrape down to bare metal, because that damages the surface; do not clean the cut face if the new pane is going straight in; remove the spacer tape completely; and re-bond only with a material approved by the adhesive manufacturer for that substrate.
Then comes the part that decides the programme. Before the temporary clamps holding the new pane can come off, adhesion has to be verified on test specimens and the bead has to be cured right through. The same published guidance gives the clamp removal point as seven days for two-component adhesives and twenty-one days for one-component adhesives, and states that the weather seal goes on only after the structural adhesive has fully cured.
| Scenario | Access needed | Time before the pane carries load | What it means for an occupied building |
|---|---|---|---|
| Beaded unit, ground floor | Interior, hand tools, two people | Same visit | A maintenance line item |
| Bonded unit, ground floor | Trained crew, suction lifter, clamps | Seven days with a two-part adhesive, twenty-one with a one-part | The opening is a work zone for one to three weeks |
| Bonded unit, upper floor or tight site | Specialist access equipment in addition to the glazing crew | Same cure clock, plus access set-up and strip-out | Access plant is often the largest single line on the invoice |
Field bonding is held to a tighter standard than shop bonding for a reason the guideline states plainly: the site is dirty and the cure conditions are not controlled. Surface preparation, primer, joint dimension and cure time all follow the written procedure, and if the bond is in doubt, the instruction is not to glaze it.
The seamless question and the weight question are the same question, because the weight is what makes the removal method matter. Our arithmetic, on the published maximum sash:
Two things follow. First, whoever takes that panel out is handling a glass unit in the region of two hundred kilograms, which is a suction lifter and a second person at minimum, and a crane or a spider machine on an upper floor. Second, we publish no load or driving capacity for this series. We do publish a driving capacity of 220 kilograms for a different heavy-duty sliding series and a 400 kilogram twenty-wheel carriage for another, and those two figures are not the same measurement and neither of them transfers here. Do not sort them into one column and read down.
The 75 mm variant publishes a 27A insulating glass with inert gas filling, which is a wider cavity and the same order of glass weight. A wider cavity does not make the pane lighter; it makes the unit thicker and the handling no easier.
This is the part that is specific to a thermal break door, and it is the reason the two words in the title do not sit comfortably together.
A thermally broken aluminium profile is not one piece of metal. Polyamide strips, in our case PA66GF25, physically split the extrusion into two separate aluminium halves so that conducted heat cannot travel straight through. Published thermal conductivities for that comparison are stark: polyamide with 25 percent glass fibre sits at about 0.30 W/(m.K) against roughly 160 W/(m.K) for aluminium, and aluminium is routinely described as conducting around a thousand times faster than timber.
Now put a welded corner next to that. Welding fuses aluminium to aluminium. It cannot fuse polyamide to aluminium, and it cannot reach the inside of a hollow extrusion where the profile actually carries load. So on a thermally broken profile, a corner that looks seamless from outside is, by construction, seamless on one shell only. The other shell is still joined mechanically, and the strip that makes the door a thermal break door is the one component in the corner that no welding process touches.
There is a second, more awkward point, and it comes from a Chinese architectural hardware maker arguing against the practice on its own pages. Their description of the seamless welding sequence is that it runs in reverse to the conventional one: assemble, weld the outside mitre, grind it flat, and only then powder coat. Their objection is that domestic coating lines run above 200 degrees and are hard to control, and that a polyamide strip carried through that line loses strength. Whether that applies to any given factory depends entirely on whether the strip is in the profile during coating. It is a fair question to ask of anyone selling you a welded thermal break frame, including us.
To be clear about scope: we publish pressure-line-free for this series. We publish nothing about how the corners are made. The three positions below are the industry context you need in order to ask the question, and we are not going to adjudicate between them.
| Who is speaking | What they say | Why a buyer should care |
|---|---|---|
| A Chinese door and window maker's selection guide | Welding achieves molecular-level fusion and makes the frame one piece; overall strength is described as more than three times that of conventional crimped and injected corners, with better air, water and wind performance | This is the sentence most buyers read first, and it is a marketing sentence |
| A Chinese architectural hardware and fittings maker, publishing its own press test | The seamless welded corner deformed and cracked at 682 newtons; the pin-and-injected crimped corner did not deform or open until past 1749 newtons. Their conclusion in one line: it looks better, and that is the only point | A party with commercial skin in the game saying the thing that costs them. That is why it is worth reading |
| A Chinese industry commentary on material and process standards | Laser welding genuinely solves the strength problem of very narrow frames, frames of twenty to thirty millimetres, and is now common on premium minimal-frame lines; the two processes are not a replacement relationship, they suit different applications | The only one of the three that names a condition under which welding is the right answer |
The two numbers in the middle row are about two and a half times apart. Note also where the disagreement sits: the marketing claim is about the whole frame, the test is about the corner, and the commentary is about narrow frames specifically. Three people can each be right about a different object, which is exactly why the question has to be asked with the object named.
It is not only an aesthetic. There are four real gains, and one of them is barely ever priced.
| Thing people hope it improves | Reality |
|---|---|
| Air, water or wind ratings | Those are measured on a whole tested configuration. We publish no such rating for the sliding door range, and removing a bead does not create one |
| Thermal performance | A K value belongs to a specimen, not to a series. We publish no K value for the sliding door range, and the bead is not the term that would move it most |
| Load capacity | Capacity is a function of the roller carriage and the gear, not of whether a bead is present. Nothing published here |
| The water line at the floor | That is the 8 mm low track versus the 43 mm high track. Seamless does not move either number |
| How much glass you can see | That is decided by sash width and by the meeting stile, discussed next |
| How heavy the panel is | About 195 kilograms of glass on the largest published sash, whatever holds it in |
Here is the arithmetic that should sit next to any seamless claim on a sliding door. Two panels meet in the middle of the opening when the door is closed. At that point the eye is not looking at one sash stile, it is looking at two, side by side.
| Feature | 96 mm variant | 75 mm variant | Compared with the 36 mm outer frame |
|---|---|---|---|
| Visible band where two panels meet | About 192 mm | About 150 mm | About five and a third times, and about four and a seventh times |
| Can it be designed out | No | No | The overlap is where the lock, the seal and the anti-lift geometry have to live |
So the honest framing is this: the seamless claim is about a 36 millimetre member, while the visual band you cannot remove is more than five times wider on the 96 mm variant. That is not a criticism of the product, it is the geometry of a sliding door. It is also why the 75 mm variant exists, and why the word narrow in a sliding door specification should always be followed by a question about which member is being narrowed.
The opposite extreme is worth naming too. If what you actually want is an elevation made of many narrow vertical elements, the honest product is not a slimmed sliding door. Options such as bi fold louver doors are built out of seams on purpose, and they are a different product family entirely, one we do not list.
Every seamless conversation should end with a removal conversation, and a removal conversation on a sliding door starts with a number that is almost never published: the head clearance.
A sliding panel comes out by being lifted into the head channel until its bottom clears the bottom rail, then tilted in. To clear the 43 mm high track, the panel has to rise at least 43 mm. To clear the 8 mm low track, it has to rise 8 mm. We publish both track heights and we do not publish the head pocket depth that has to accept that lift. Ask for it, and ask it before the head detail is set, because it is the number that decides whether the panel can leave the frame at all.
There are three further points that belong in the same conversation:
If the opening is small, internal, and the door will never need to be de-glazed in place, none of this matters and you should not be reading this section. A wet room or a compact utility opening is better served by a simpler product, and bathroom doors folding is the kind of answer we would point you to before we pointed you to a 182 mm three-track frame. We do not list one.
| Situation | Why this is the wrong product | What to look at instead |
|---|---|---|
| Glass must be swappable in one visit, in place, repeatedly | That is what a removable bead is for, and this series is published as pressure-line-free | Ask for a beaded sliding series and say so on the order |
| Upper-floor hotel or apartment with no external access | A bonded unit needs a crew, clamps and a cure window in an occupied room | Resolve the retention method and the access plan in writing before ordering |
| The opening is a garage or a personnel door | That is a hinged door, with a completely different load path and a different set of rules | Look at hinged options such as swing door garage doors. Our own swing door pages currently carry no products, and we would rather say that than sell you the wrong thing |
| You need a genuinely flush floor with no upstand | The low track is 8 mm, not zero, and the drainage has to go somewhere | Treat it as a slab and waterproofing decision, and involve the engineer early |
| The wall is already built and the reveal is fixed | 182 mm of frame depth has to go somewhere, and it is a series property, not an adjustable one | Check the two-track 126 mm version, or a different series, against the built condition |
| You want a written air, water or wind rating from the catalogue | We do not publish one for the sliding door range | Ask for a calculated value for your exact opening and glass build-up, under a named standard |
The right-hand column is the point of this table. A gap is not a defect; it is usually a piece of information that belongs to your building rather than to our factory. But it needs to be named before the order, not after.
| Item | Published by us | You must request | Why the gap exists |
|---|---|---|---|
| Glass retention method | Only that it is pressure-line-free | Which of the three families replaces the bead, and the written removal procedure | It is the highest-value unpublished fact on this product |
| Glass pocket depth | Sash thickness 55 mm, not the pocket | The rebate dimension off a section drawing | Thickness is a stack-up; the pocket is a different measurement |
| Head clearance for panel removal | Not published | The lift available above the panel, against the 43 mm and 8 mm tracks | It depends on the head detail, which is decided on site |
| Load or driving capacity | Not published for this series | A capacity for your sash size and glass build-up, with the measurement defined | It is a function of the glass, and the glass is not fixed yet |
| Maximum sash size | 2500 by 3000 mm for one variant only | The size for your variant, and the glass build-up it assumes | The published maximum is conditional on a glass weight nobody prints |
| K value | Not published for the sliding range | A calculated value for your size, your glass and a named standard | A thermal figure belongs to a specimen, not to a series |
| Air, water and wind performance | Not published for the sliding range | Test report, standard name and version, and whether the specimen was the opening configuration | A fixed panel almost always tests better than a moving one |
| Corner construction | Not published | Welded, crimped, injected, or a combination, and in what sequence | It decides the coating sequence, which matters on a thermal break profile |
| Coating batch plan | Standard colours named, custom matching available | One batch across the whole project, with batch numbers recorded against panel marks | Batches are a production fact, not a catalogue fact |
| Spare parts schedule | Not published | Rollers, gaskets, seals, locks, handles, touch-up material, shipped in the original container | The freight argument has to be settled once, at the beginning |
| Opening size and anchorage | Not published | Your opening in millimetres, the anchorage layout, the drainage route and the panel sequence | They are yours, not ours. We cannot publish what we do not own |
| Project approval | Not published | Evidence, drawings, sections and test pieces from us; the approval itself from your authority | Approval is issued to an applicant for a tested configuration. It does not travel with a series name |
| Line | What a good entry looks like | What happens if it is blank |
|---|---|---|
| Glass retention method | Named: bead, sash-assembled, or adhesive bond | You find out on the day the glass breaks |
| Written glass removal procedure | A document, not a description | The method gets improvised on site, which is where bonds fail |
| Opening in millimetres | Width, height and the head clearance, measured at three points | Nobody knows whether the panel can be lifted out |
| Wall build-up, outside to inside | Every layer named, because 182 mm has to fit somewhere | The frame depth becomes a site problem |
| Track choice | 8 mm or 43 mm, chosen against the floor levels and the weather exposure | The flush floor arrives and the water has nowhere to go |
| Glass build-up | Exact make-up and total glass thickness in millimetres | Every size and every capacity figure is unanchored |
| Panel count and sequence | Which panels move, which are fixed, and the removal order | The fixed panel turns out to be the one that has to come out |
| Screen specification | Mesh type, colour, panel arrangement | A second panel arrives undefined in the same opening |
| Colour and batch plan | One coating batch for the whole project, recorded against panel marks | A replacement panel in three years does not match |
| Hardware set | Named components, not a brand name alone | A brand is not a parts list when something fails |
| Spare parts shipped with the order | An itemised list, in the original container | The freight of one roller becomes a dispute |
| Performance evidence | Standard name, version, and the configuration tested | A rating without a standard is an adjective |
| Who signs for the opening and the perimeter sealing | A named party, in writing | Water appears and four trades each have a document saying it is not theirs |
| Freeze date for changes | A date in the contract, not a lead time | A change at the assembly stage costs labour, and after that costs a second shipment |
| Ask this | An answer that sounds reasonable and tells you nothing |
|---|---|
| How is the glass held in without a pressure line? | It is a seamless system, very advanced |
| Can the glass be replaced without removing the frame? | Of course, any glazier can do it |
| What is the head clearance above the panel? | It is standard, the panel always comes out |
| Is this frame seamless welded? | It is seamless, yes |
| What is the load capacity for my sash size? | It is heavy duty, four hundred kilograms |
| What is the K value for this door? | The series is very energy efficient |
| Which standard was the performance tested to? | It meets international standards |
| Was the tested specimen the sliding configuration? | The series is tested |
| Will everything be the same colour? | It is all the same colour name |
| Who signs for the perimeter sealing? | The installer handles all of that |
No. On this series it means the glazing bead, the pressure line, has been designed out. It says nothing about the corner joint, and on a thermally broken profile a corner can only ever be seamless on one of the two aluminium shells, because the polyamide strip that makes it a thermal break cannot be welded.
Not necessarily, and published opinion is genuinely divided. One Chinese maker claims more than three times the strength of a conventional crimped and injected corner. A Chinese architectural hardware maker publishes a press test in which the welded corner deformed at 682 newtons while the crimped and injected corner held past 1749. We publish nothing about the corner construction of this series, so we are not going to answer on its behalf. Ask, and ask which object the answer is about.
It depends entirely on the retention method, which is the one thing we do not publish. With a bead it is a glazier with hand tools in a single visit. With a structural bond, a sealant manufacturer's published procedure requires cutting the pane out, preparing to a written standard, re-bonding, clamping, and waiting seven days for a two-part adhesive or twenty-one days for a one-part before the clamps come off.
No. It is the three-track frame wall width, the depth the frame occupies inside the wall, and it is invisible once the door is installed. The two-track version of the same series is 126 mm. The visible outer frame member is published as 36 mm and the visible sash face as 96 mm or 75 mm depending on variant.
Not from a door supplier alone. We publish a low track at 8 mm and a high track at 43 mm. A flush threshold moves the water problem from the product into the slab, the membrane and the drainage, and that decision belongs to your engineer and your waterproofing designer, and it has to be taken before the slab is poured.
Because a performance number belongs to a tested configuration with a stated size, a stated glass build-up and a named standard. Printing a family value here would be a sentence about a specimen that is not your door. We would rather give you the section drawing and a calculated value for your opening than a number you cannot defend in a submittal.