Dual-colour powder coating is usually sold as a decoration option: one colour for the street, another for the living room. That is true, and it is also the least interesting thing about it. The more useful answer is that a two-colour finish is only possible on a window built a particular way, and asking for it is one of the fastest ways to find out how a factory actually assembles its profiles. We have covered what powder coating is and how it behaves on a sliding line elsewhere on this site; this piece starts where that one ends and looks at the two-face question specifically.
Below: why the thermal break is the reason dual colour exists at all, why one kind of thermal break cannot do it, what the finish does not change, why a dark exterior is a thermal specification rather than a taste, which parts of a window can actually be two colours, why the decision becomes irreversible at the moment the profile is crimped, and how to write all of that into a schedule.
If you read only one paragraph, read this one. The advantage of a dual-colour finish is that a single window can answer to two different authorities without either of them losing. The outside of a building is almost never chosen by the person who chooses the inside. A developer's elevation drawings, a homeowners' association palette, a heritage streetscape or a neighbouring facade sets the exterior colour; the interior is set by joinery, wall paint, flooring and how much light the room needs. With one colour, one of those two briefs gets compromised. With two, neither does.
That is worth more than it sounds, because the alternatives are all more expensive. Changing the extrusion to alter how a facade reads costs millimetres of aluminium and a new die. Cladding or lining the inner face costs a second trade on site. Choosing a deeper or slimmer section to change the look costs structural and thermal work. A second powder batch on a face that is already going through the line costs a fraction of any of those, which is why it is usually the cheapest way to change how a whole elevation reads.
Powder coating cannot put two colours on one continuous piece of metal. There is no masking process that will hold a clean line along the length of an extrusion at production speed and survive the abrasion of a building site. So the only way to get two colours on one frame is for the frame to be two pieces that are joined later.
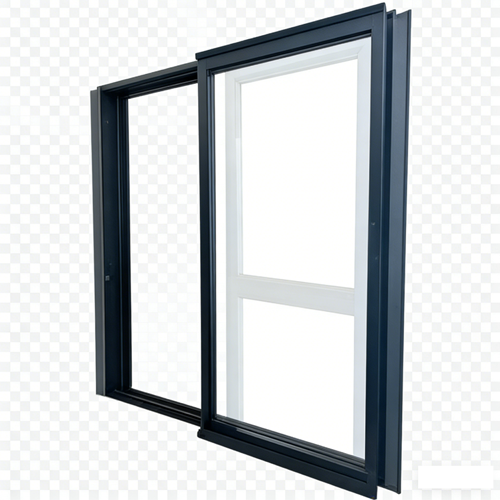
A modern thermally broken profile is not one extrusion. It is three components: an outer aluminium shell, an inner aluminium shell, and a polyamide strip that joins them and carries the load between them. The two shells are separate pieces of metal until they are rolled onto the strip. That separation is exactly what makes two colours possible - the outer shell is coated in one colour, the inner shell in another, and only then are the three parts crimped into a single profile.
Every ALPES window and door series described in our product documentation is built this way, on PA66GF25 polyamide strips with 6060-T66 aluminium at 1.8 mm to 2.5 mm depending on the series. The C116 casement runs 34 mm to 44 mm multi-chamber strips.
Here is the part that rarely gets written down, and it is the real answer to the question in the title. Not every thermal break is a three-part construction. The older method - known in the trade as pour-and-cut - starts with a solid aluminium extrusion, cuts a channel through it and pours in a liquid resin that is later bridged. The result is thermally broken, but it is still one piece of metal. Because it is one piece of metal, it cannot be powder coated in two colours. Finishing houses that describe the process publicly are blunt about this: the polyamide strip is what made dual-colour powder coating simple, and before it the only way to get two colours was to powder coat one face and apply a decorative film to the other.
There is a structural reason to care about this too, not just a colour reason. BS EN 14024:2023 classifies thermally broken profiles by how they transfer load. Type A is a mechanical interlock - a polyamide strip pressed into a knurled aluminium groove - where shear is transferred by the interlock and a shear failure does not significantly reduce transverse tensile strength. Type B is a cast or adhesive barrier, where a shear failure does weaken the section badly. The construction that lets you have two colours is the same construction the standard treats as the more forgiving one. Asking "can I have two colours?" is, in practice, asking "is this a Type A polyamide strip profile?"
Single-colour production and dual-colour production are not the same route through the factory. A single-colour length is often crimped in mill finish and coated afterwards as a complete profile. Published technical manuals for thermally broken systems show that route and put a hard ceiling on it: the curing oven runs at roughly 190 to 200 degrees Celsius, and the guidance warns that exceeding 200 degrees can affect the mechanical stability of the polyamide. The strip is in the oven during that cycle.
Dual colour reverses the order: coat the two shells separately, then crimp. The strip never sees the oven, which is one reason the route is viable at all. But it also means the crimp now happens onto an already-coated surface, in a channel whose knurl geometry was designed to bite into bare aluminium. That is not a reason to avoid dual colour - it is a reason to ask one specific question: was the shear and transverse tensile value measured on a coated, crimped sample, or on a bare one? EN 14024 gives you the vocabulary to ask it properly, and AAMA 505 covers the same ground through thermal cycling and dry shrinkage testing.
It is worth being clear about the things a second colour cannot do, because they are the things buyers quietly hope it will.
The most common dual-colour combination is a dark exterior with a light interior, and it is the one that deserves the most scrutiny, because the two faces now live in genuinely different thermal environments.
A dark coating absorbs more solar radiation than a light one. On a west-facing elevation in a hot climate, the outer shell reaches a surface temperature far above the ambient air while the inner shell stays near room temperature. That temperature difference sits across precisely the component that holds the window together: the polyamide strip. Published specifier guidance for hot-climate projects makes three points that are worth repeating here. First, the barrier should be tested at a temperature category that matches the elevation - EN 14024 defines temperature categories for exactly this reason, and the high-temperature category is the one to ask about when the outside is dark. Second, large dark leaves move measurably between morning and late afternoon, so lock keeps, clearances and seals need to allow for it. Third, shading beats coating: an overhang that keeps direct sun off a dark west-facing door removes the heat input at source, which no powder can do.
The coating itself also has to be graded for it. Durability schemes for architectural powder - Qualicoat classes and the AAMA 2603, 2604 and 2605 tiers - are defined by natural weathering exposure and gloss retention, and the classes are not interchangeable. Saturated dark colours show chalking and fading far more visibly than a pale one, so the exterior face is where the higher class earns its keep. Infrared-reflective dark powders exist and can lower the surface temperature of a dark frame while still looking dark; if you go that route, check the durability class alongside the reflectance, because a cooler coating in a lower class is not automatically the better choice on a sun-facing wall.
Dual colour is one of several answers to "the outside has to be one thing and the inside another". It is not always the right one.
| Approach | How it works | What it costs | Where it fails |
|---|---|---|---|
| One compromise colour | A mid tone that is acceptable from both sides. | Nothing. Fastest and cheapest. | It satisfies neither brief. On a large elevation the compromise is visible every day. |
| Dual-colour powder coating | Inner and outer shells coated separately, then crimped onto the strip. | A second coating run and a longer production sequence. | Irreversible once crimped, and only available on polyamide strip profiles. |
| Interior lining or cladding | The inner face is covered by a second trade after installation. | On-site labour, joints at every corner, and a detail that has to be drawn. | Joints open, linings trap condensation, and the reveal still shows the exterior colour at the edges. |
| Wood-grain sublimation on the inner face | A printed finish transferred into the coating on one face. | Comparable to a second colour, sometimes less. | Sublimated inks are more UV-susceptible than solid pigments. It belongs on the room side, not on the weather side. |
This is where most dual-colour orders go wrong. "Dual colour" is agreed in an email, and then nobody says which components the split applies to. A window is not one profile; it is a family of profiles, and some of them are seen from both sides at once.
| Part | Who sees it | Can it be split | What to write in the schedule |
|---|---|---|---|
| Outer frame | The street | Yes, this is the classic split | External colour code and gloss level |
| Inner frame | The room | Yes | Internal colour code and gloss level |
| Sash | Both, at once | Yes, if the sash is itself thermally broken | State explicitly that the split applies to the sash, not only the frame |
| Mullion or transom | Both | Usually yes | Ask for the visible face dimension as well as the colour |
| Glazing bead or press line | The room, in almost every operable system | No need - it is interior only | Must be the interior colour. This is the piece most often delivered in the exterior colour by mistake. |
| Insect screen | The room on an outward-opening window; may be external on some sliding configurations | No | Name the screen colour as well as the mesh specification |
| Handle and hardware | The room, mostly | No - one colour only | Handle finish is a separate line item, and the finish grade matters on coastal projects |
| Threshold and track | Both, and walked on | Ask - it spans the full frame depth | Confirm whether the track is coated as one length or split, and check the drainage detail alongside it |
| Couplers, bay poles and structural joints | Often both | Depends on the part | On long coupled runs, ask which colour the coupler arrives in before the elevation is built |
One practical aside about the interior face: it is the face that gets touched. A kitchen casement window is opened and wiped more often than any other window in a house, and a dark matte interior shows every fingerprint and every splash of cleaning product while a light one hides them. If you are fitting tilt and turn window blinds on the sash, the blind and the inner face are the only two things you see from the room - so those two should be chosen together, not in separate meetings.
Here is the cost that almost never appears in a quotation, and it is the one that should carry the most weight in the decision.
A single-colour profile that has been coated in the wrong shade can be stripped and re-coated. A dual-colour profile cannot. Once the two shells have been crimped onto the polyamide strip, pulling them apart destroys the strip and the length is scrap. Coating houses that publish their process say this plainly. What follows from it is simple but easy to miss: the moment of crimping is the moment the colour decision becomes permanent. There is no rework and no second attempt.
Four consequences are worth planning for before the order goes in.
"Dual colour, grey outside and white inside" is not a specification. This is.
| Line to write | Why it decides something | A useless answer looks like |
|---|---|---|
| Both colour codes, plus an approved physical chip for each | Colour names mean different things to different people | "Standard grey" |
| Gloss and texture for each face separately | The same colour reads differently at different gloss levels, and the two faces have different jobs | "Same as our standard finish" |
| Which parts the split applies to: frame, sash, mullion, bead, screen | Without this, the bead and screen arrive in whichever colour is easier to run | "Dual colour as discussed" |
| Confirmation of a polyamide strip thermal break, with the strip material and width in millimetres | No strip, no dual colour, and a Type A interlock is the construction you want anyway | "Thermally broken profiles" |
| Characteristic shear and transverse tensile values to EN 14024, measured on a coated and crimped sample | Dual colour changes the assembly sequence, so the mechanical value has to be proven on the actual route | A test report for a bare profile, or a different series |
| The temperature category the barrier was assessed at, if the exterior face is dark | EN 14024 defines temperature categories for a reason; a dark west elevation lives at the top of that range | "Tested to European standards" |
| Coating standard and class for the exterior face, plus film thickness | Chalking and fading show far more on a saturated dark colour than on a pale one | "High quality architectural powder" |
| An approval sample: a cut corner of the crimped profile showing both faces | After crimping there is no rework. This is the last point at which you can change your mind | A photo, or a separate sample of each colour |
| Spare lengths, and both batch numbers recorded on the delivery documents | A year-eight replacement has to match both faces from both batches | Nothing, until you need it |
| The additional production time, stated in writing for this order | Two runs and a reversed sequence take longer, and the number depends on your colours and quantities | "Normal lead time" |
Being straight about the boundary here saves everyone time. ALPES publishes a standard palette - Ice Cream White, Aurora Gray, Starry Sky Gray and Brown Coffee - and lists custom colour matching as available. Dual-face finishing falls under custom matching, so it should be confirmed against your specific order rather than assumed to be a standard capability of every series. What we can say without qualification is that the construction that makes it possible is there: every series in the range is a 6060-T66 aluminium profile on a PA66GF25 polyamide strip, which is the three-part, Type A arrangement described above.
| Item | What is published | What you still have to ask for |
|---|---|---|
| Standard colours | Ice Cream White, Aurora Gray, Starry Sky Gray, Brown Coffee | Which of these can be produced on both faces of the series you are buying |
| Custom matching | Available on request | Minimum quantity per colour, and the effect on production time |
| Profile and strip | 6060-T66, 1.8 to 2.5 mm by series, PA66GF25 strips; C116 runs 34 to 44 mm | EN 14024 characteristic values for your series, on a coated and crimped sample |
| Thermal values | System K values: AW90 1.3, C120 1.6, C116 1.7 | A whole-window figure for your sizes and glass build-up. These are system values, not NFRC-rated whole-window values, and the sliding and side-press series do not publish a K value at all |
| Mechanical and corrosion tests | AW90: 5,000 N shear resistance, 240-hour salt spray | The equivalent figures for the series you are ordering. The AW90 results are published test results for that series; they are not a project qualification and they do not transfer to another series |
| Coating standard | Not published as a scheme class | Name the class you need - a Qualicoat class or an AAMA tier - and ask for the certificate against it. Do not assume a grade because the price looks right |
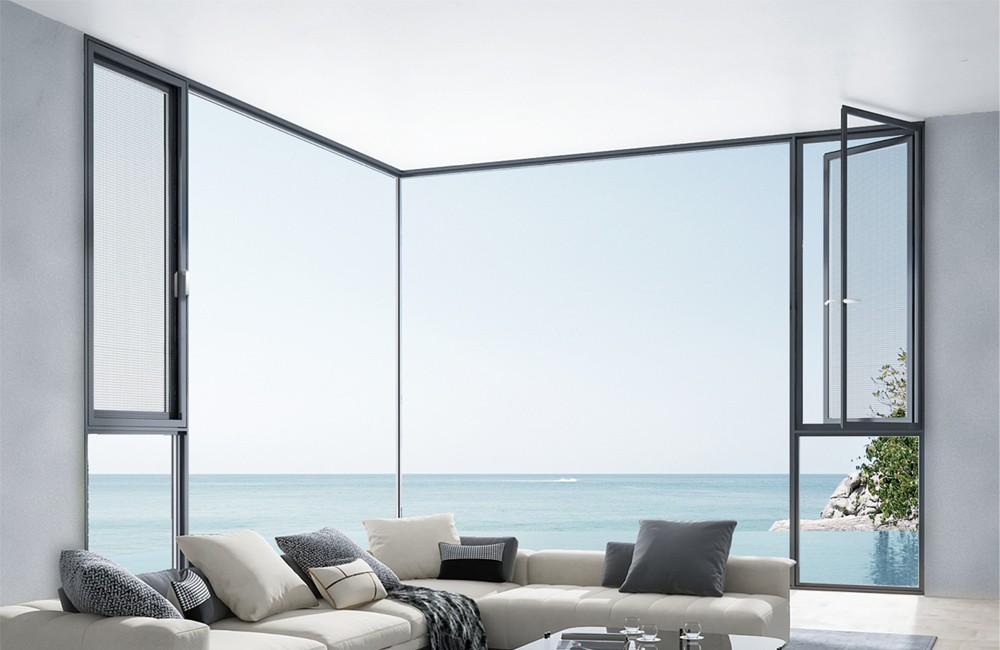
On the inward-opening side of the range, the dual-face question comes up most often with tilt and turn window designs such as the AW90, where the inner face is the one you live with and the outer face belongs to the elevation. The same logic applies wherever the room and the street genuinely want different things; where they do not, a single colour is still the faster and more forgiving answer.
No. The coating film is measured in microns and the thermal work is done by the polyamide strip and the chamber geometry. What does change is the temperature the outer shell reaches if you choose a dark exterior, and that is a question for the barrier's tested temperature category, the coating class and the shading, not for the published K value.
They live different lives. The exterior face takes UV, rain, salt and temperature cycling; the interior face takes handling, cleaning products and knocks. That is a good argument for putting the higher coating class where the weather is and choosing the interior colour for how it wears under hands rather than under sun.
Not on a dual-colour profile. A single-colour length can be stripped and re-coated; once the two shells have been crimped onto the polyamide strip, separating them destroys the strip. Approve a physical sample of the crimped profile before production, and order spare lengths.
It is a specification decision rather than a mistake. A dark coating absorbs more solar radiation, the outer shell runs hotter than the inner one, and that difference sits across the thermal break. Ask for a barrier tested at the high temperature category, specify a coating class graded for saturated dark colours, allow for movement in the hardware and seals on large leaves, and add shade where you can.
They cannot be two-tone, so they have to be given a colour deliberately rather than by default. On an outward-opening window the screen sits on the room side and should be the interior colour. The handle is a separate line item with its own finish, and on a coastal project the hardware finish grade matters as much as the frame coating.
Record both colour codes, both gloss levels and both batch numbers in the building file at handover, along with the series and the profile drawing. A replacement ordered from a colour name alone will not match, and with two faces there are two chances to get it wrong.
The honest summary is that dual-colour powder coating is a small decision with a long memory. It costs less than any other way of reconciling a facade brief with an interior brief, it tells you something real about how the profiles are built, and it cannot be revised after the crimp. Get the two colour codes, the two gloss levels, the list of parts the split applies to and one physical cut-corner sample agreed before production, and it will still be right in twenty years. Leave any of those four open, and you will find out about it when the container is already on the water.
If you are working on an elevation now, send the opening schedule with the exterior and interior colour requirement marked on each line, and ask for a dimensioned finish specification and an approval sample for each profile type. You can reach the team through the ALPES contact page with your drawings attached.