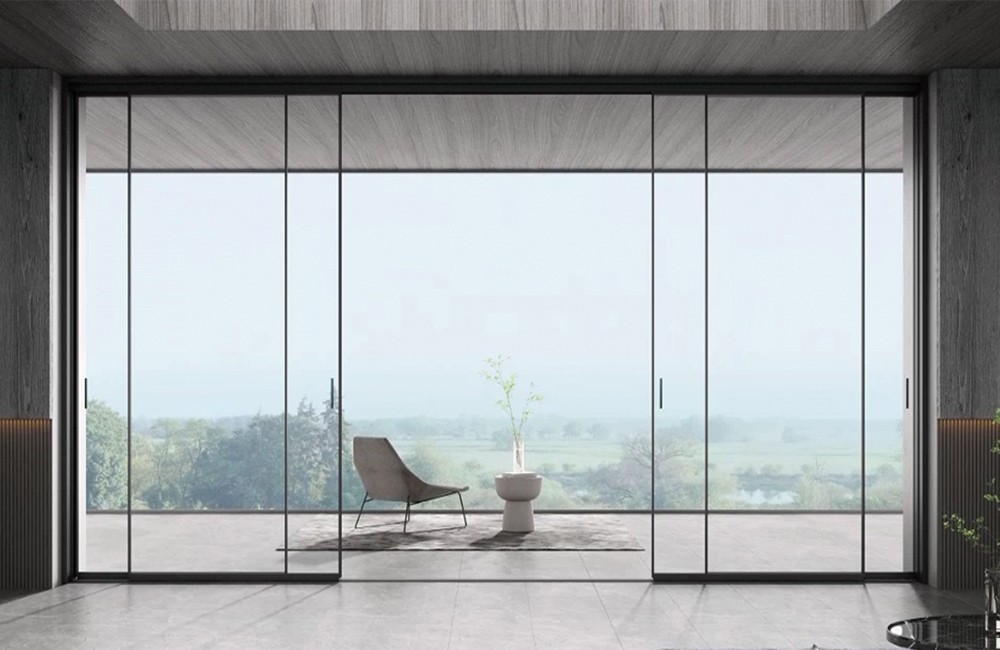
The phrase SL126 thermal break sliding door 6060-T66 aluminum reads like the name of one product. It is not. It is three claims, made by three different parties at three different moments, and only one of them is a claim about the door you will actually receive.
That matters because the third noun — the alloy and temper — is the one most often used as a reason to choose. It is also the one that carries the least decision. In this catalogue, 6060-T66 is printed on every series. A line that is identical across all ten products cannot be the reason you pick one of them.
| The noun in the title | What it actually answers | Who decides it | When it becomes irrelevant |
|---|---|---|---|
| SL126 | Which extrusion family, how many tracks, how wide the meeting stile is | The system house, long before your project exists | The moment you write "SL126" without the suffix and without the track count |
| thermal break | Whether the inner and outer halves of the frame are joined by metal or by polyamide — and how wide that joint is | The rolling line that knurls, inserts and crimps the composite profile | When the strip width is not published and no frame calculation is offered |
| 6060-T66 | What the billet and the press did — a guaranteed floor on strength, achieved by a process | The extrusion plant, and the oven that follows the press | Every time someone offers it as the reason to choose one series over another |
None of this makes the alloy unimportant. It makes it a floor rather than a differentiator, and a floor is exactly the kind of number that should be verified rather than marketed. This article works through what each of the three nouns commits to, where each commitment stops, and which two lines on the SL126 page carry the decisions that 6060-T66 does not.
6060 is an aluminium–magnesium–silicon alloy in the EN AW numbering system, with its composition set by EN 573-3. It is a general extrusion alloy: alloy datasheets describe it as suitable where no special strength is required, with very good surface quality and good response to coating, and they list windows and doors, facade construction and architectural trim among its typical fields.
T66 is not a stronger metal. It is a temper designation, and the definition from EN 515 is worth reading in full because it says something most spec sheets do not:
So the difference between T6 and T66 is not chemistry. It is what happened on the press, how fast the section was quenched coming off it, and what the ageing oven did afterwards. That is a claim about equipment and process control, which is precisely why it cannot be checked with a tape measure.
Here is what the guarantee looks like in numbers. These are the minimum values published for EN AW-6060 extruded profiles, taken from alloy datasheets and from a European system-house technical table that cites EN 755-2:
| Temper | Wall thickness band | Tensile strength Rm, minimum | Yield strength Rp0.2, minimum | Elongation, minimum | Brinell hardness, typical |
|---|---|---|---|---|---|
| T5 | up to 5 mm | 160 MPa | 120 MPa | 8 percent | about 60 |
| T6 | up to 5 mm | 190 MPa | 150 MPa | 8 percent | about 70 |
| T66 | up to 5 mm | 215 MPa | 160 MPa | 8 percent | about 75 |
| T6 | 5 to 25 mm | 170 MPa | 140 MPa | 8 percent | about 70 |
| T66 | 5 to 25 mm | 195 MPa | 150 MPa | 8 percent | about 75 |
Two cautions before you use that table. First, published tables quoting the same standard do not agree in every cell: one quotes elongation on a 50 mm gauge length at 6 percent where another quotes 8 percent, and every datasheet we found marks the hardness column as indicative only. Read the table as the shape of the standard, not as your acceptance values. Second, and far more important for this particular door:
Two conclusions follow. T66 buys roughly 25 MPa more guaranteed tensile and 10 MPa more guaranteed yield than T6 in the same alloy — a raised floor, not a different material. And the guarantee is banded by wall thickness, which means the wall thickness is where the real specification lives.
Here is the uncomfortable part of putting an alloy temper in a product title: nothing about it can be confirmed on site.
Extruders publishing on their own process control describe the verification ladder clearly. Mechanical testing — yield strength, tensile strength, elongation — is the final validation and is what the standard requires. Hardness testing, Brinell or Vickers, is described as a fast screening tool used during production. Microstructure inspection sits above both, used on higher-end projects: cut, polish, etch, and look at precipitate shape and distribution.
A hardness reading is useful and it is not proof. Both directions of error look the same from the outside. Under-ageing leaves fewer precipitates and the yield strength drops. Over-ageing coarsens the precipitates and strength falls again while ductility rises. A single number on a handheld gauge cannot tell you which one you have, whether the sample came from the batch you received, or what the gauge was calibrated against.
One published account makes the risk concrete: a construction client received profiles marked T6, several beams bent under light load during installation, and re-testing found mechanical strength closer to T4. The stated cause was heat-treatment control. The marking was correct on the label and wrong in the metal.
So the practical question is not "is it T66" but "what document will you accept". The vocabulary for that exists and is widely used:
What not to accept is the sentence "our profiles are 6060-T66" with nothing behind it. On a sash that can be 3.0 metres tall, that sentence is not a specification. It is an adjective.
This is the part of the alloy conversation that almost never appears in a window article, and it is the part that connects 6060-T66 to the geometry of a very tall sash.
The EN AW-6060 datasheet has a section on weldability. It lists gas welding, TIG and MIG ratings, recommends filler materials, and then says this: due to the heat input during welding, the mechanical properties will be reduced by approximately 50 percent, with a reference to EN 1999-1.
Now think about where a sliding sash collects its worst loads. Not in the middle of the glass. At the four corners — where the stile meets the rail, where the roller loads come up into the bottom rail, where the lock drive runs, where the wind suction on a 7 square metre panel resolves into the frame.
That is why "what is the corner construction" is a legitimate, specific question, and why the alloy line at the top of the page does not answer it. The families of answer, with their trade-offs stated honestly:
| Corner method | What it does to the temper | What it buys | What it costs |
|---|---|---|---|
| Injected corner brackets with structural adhesive | Preserved — the extrusion stays continuous | Keeps the declared mechanical properties through the joint; seals the joint at the same time | Depends on adhesive quality and on the process being followed, not just specified |
| Crimped or mechanically keyed corners | Preserved | No heat, repeatable, inspectable | Crimp quality is a tooling and maintenance issue; a tired tool produces a tired corner |
| Welded and dressed corners | Substantially reduced in the heat-affected zone | The cleanest visual line; can produce shapes the other two cannot | The published temper no longer describes the corner |
SL126/182(96) is published with a seamless, pressure-line-free frame; the (75) variant is published as a 38 mm slim frame with the same pressure-line-free approach. Neither description says how the corner is made, and neither should be read as a claim about it. Ask, and ask for the section drawing that shows the answer.
SL126 is published at 2.0 mm profile thickness with local reinforcement to 3.0 mm in critical areas. The (75) variant states it as locally reinforced up to 3 mm wall thickening.
This is the most useful line on the page and the least discussed, because it is two statements wearing one sentence:
A sash 3.0 metres tall does not load its section evenly. Where the thickening starts and stops is the output of a calculation, and it is the only part of the wall-thickness story that changes between a door that works and a door that creeps.
GB/T 8478-2020 makes two statements about wall thickness, and the order matters.
The first is that the nominal wall thickness of the main load-bearing profiles for exterior doors and windows shall be determined by design calculation and testing. The second is a table of minimum nominal values, expressly excluding the fin walls at accessory functional grooves.
Public sources quoting that second part do not agree with each other. One set of public summaries gives exterior doors 2.0 mm, interior doors 1.6 mm, exterior windows 1.8 mm, interior windows 1.4 mm, and auxiliary profiles 1.2 mm. A public procurement clarification quoting clause 5.1.2.1.2 gives exterior doors 2.2 mm, interior doors 2.0 mm, exterior windows 1.8 mm and interior windows 1.4 mm.
We are not going to choose between them. Two public readings of the same clause produce two different numbers for the same exterior door, and that disagreement is itself the most useful thing on this page: read the version your project adopts, and put it in the order in writing. Do not take a threshold from an article, including this one.
What matters more than either number is the first statement. "Determined by design calculation and testing" turns the published 2.0 mm into a floor and turns the 3.0 mm zones into the actual engineering. It also tells you what to ask for: not a bigger number, but a drawing with the reinforced zones marked.
PA66GF25 means polyamide 66 with 25 percent glass fibre. Strip manufacturers publish their performance against GB/T 23615.1, and the table is more interesting than most buyers realise.
| Property (GB/T 23615.1) | Published value | Why that row exists |
|---|---|---|
| Density | about 1.3 g per cubic centimetre | Roughly half the mass of the metal it replaces |
| Coefficient of linear expansion | 2.3 to 3.5 times ten to the minus five per kelvin | The band starts at the expansion rate of aluminium. This is the reason for the material, not a bonus. |
| Vicat softening temperature | not less than 230 degrees Celsius | Lets the assembled composite pass through the coating cure oven |
| Melting point | not less than 240 degrees Celsius | The margin above the process temperature it has to survive |
| Tensile strength, longitudinal | not less than 80 MPa | Along the strip |
| Tensile strength, transverse | not less than 70 MPa | Across the strip — the direction the two frame halves pull apart |
| Transverse tensile after heat, cold, water and ageing exposure | not less than 45, 80, 35 and 50 MPa respectively | Four separate degradation routes, each with its own floor |
| Elastic modulus | not less than 4500 MPa | Why the composite behaves as one member under load rather than two loose ones |
| Elongation at break | not less than 2.5 percent | It has to survive the knurling and crimping that locks it in |
Three things follow, and all three change how you read the word "thermal break".
The expansion match is the reason, not a feature. Aluminium sits around 23 times ten to the minus six per kelvin. The strip's published band begins at 2.3 times ten to the minus five per kelvin — the same number expressed in different units. The composite is made by knurling the grooves, feeding the strip in, and crimping the aluminium flanges around it under pressure rollers. It then lives through decades of daily temperature cycles. If the two halves moved at different rates, that joint would work loose, and public strip guidance says exactly that, warning that materials which expand far faster decouple and leak.
The temperature rating fixes the manufacturing sequence. A working temperature around 200 degrees Celsius is quoted specifically so the assembled composite can go through the powder coating cure oven. That means the two halves are joined first and the whole assembly is finished afterwards — which in turn makes "is the coating applied before or after the strip is rolled in" a fair process question, and makes the strip's high-temperature transverse strength one of the rows that actually matters.
The transverse rows are structural, not thermal. Transverse tensile strength, plus separate floors after heat, cold, water and ageing, exist because this strip is the only thing joining the interior half of the profile to the exterior half. When it fails, the frame does not get colder. It comes apart.
The strip width for SL126/182(96) is not published. The (75) variant publishes 27A insulating glass with inert gas filling, which is a statement about the glass unit, not about the break. If you need a frame value, ask for the strip width in millimetres and the calculation that goes with it, for the size and the glass you are buying. For contrast, a wood entry door solves conduction with a completely different mechanism and hands you a completely different maintenance obligation in exchange; aluminium hands you a composite joint that nobody can inspect after assembly.
Here is the part of this catalogue that generates the most confused enquiries, because the two entries share almost everything and differ in almost nothing — and the one number they differ on is the one that decides the door's character.
| Line on the page | SL126/182(96) | SL126/182(75) |
|---|---|---|
| Frame wall width | two track 126 mm, three track 182 mm | two track 126 mm, three track 182 mm |
| Glass sash thickness | 55 mm | 55 mm |
| Frame width | 36 mm | 36 mm |
| Track heights, high and low | 43 mm and 8 mm | 43 mm and 8 mm |
| Profile thickness | 2.0 mm, locally reinforced to 3.0 mm | 2.0 mm, locally reinforced to 3 mm |
| Screen option | 80 mesh black or grey stainless steel | 80 mesh black or grey stainless steel |
| Sash width | 96 mm | 75 mm |
| Published sealing and water features | continuous four-side sealing with sealant between top track and frame; patented eave-style waterproof design; bottom track water-blocking edge; seamless pressure-line-free frame | butyl rubber waterproof gasket at frame-sash joints; multi-point locking in precision-cast reinforced casings; interchangeable drip-eave inserts; 38 mm slim pressure-line-free frame |
| Published glass note | single sash up to 2.5 m wide by 3.0 m high, about 7 square metres of daylight | 27A super large insulating glass with inert gas filling |
Everything matches except one number and the feature list. That one number — 96 or 75 — is the width of the interlock you look at every single time the door is closed, and it is also how much mechanism the section can physically hold. A wider stile can carry more locking points, a deeper handle gear, and a more generous drainage path. A narrower stile gives you more glass and less door. Neither is better; they are two different products that share a name.
And there is a second ambiguity folded into the same string. 126 versus 182 are two different frame depths, 56 mm apart, sold under one model code. Two-track and three-track are not a variation on a product; for the sub-frame, the rough opening and the structural opening they are two different products.
Writing "SL126" on an enquiry therefore specifies neither the track count nor the stile width. It is the same mistake as ordering a 36 x 80 entry door and discovering that the number on the label is a nominal call size rather than the dimension you can build to. Always write the full code — SL126/182(96) or SL126/182(75) — plus the track count and the number of panels that move.
SL126 is published with the opening method "Sliding / Lift-Sliding". That slash is carrying more weight than any other character on the page.
How lift-and-slide works, in the terms installers and system houses publish:
That last clause is the whole point, and it is the reason this section belongs in an article about an alloy.
Public thresholds exist. One manufacturer says the lift mechanism starts to be needed above about 2.4 m of sash height, and publishes lift-and-slide sashes at 2.8 m double glazed and 3.0 m triple glazed, in frames of two to six leaves. Another publishes lift-and-slide systems rated at 350 kg and 500 kg per panel, with panel heights to 3.2 m and 3.5 m respectively.
Now put that beside SL126's published maximum single sash: 2.5 m wide by 3.0 m high, about 7 square metres. Using the estimating figure the industry commonly applies — roughly 2.5 kg per square metre per millimetre of glass thickness — a 6 plus 12A plus 6 build-up is about 30 kg per square metre. Across 7 square metres that is around 200 kg of glass alone, before the profile, the hardware and any mesh are added.
That arithmetic is an estimate, not a rating, and it is not a substitute for one. But it puts a 7 square metre sash squarely on the side of the line where "sliding" and "lift-sliding" stop being a preference. When a single leaf reaches that size, the constraint is no longer the alloy, the section or even the rollers in isolation — it is whether the lift gear is rated for the leaf you are asking it to lower onto its seal. The same reasoning is why a big swing door ends up being governed by its hinges and its fixing rather than by its material.
Which makes the single most valuable unpublished number on this product the rated sash capacity of the lift gear, stated per sash and for the glass build-up you are buying. Ask for it in kilograms, ask what it was tested with, and ask what happens to the maximum panel size when you upgrade the glass — because the published maximum of 2.5 m by 3.0 m was calculated against some glass, and that glass is not named.
Maintenance guidance published for lift-and-slide is short and consistent: silicone-based lubrication of the rollers on a periodic basis, annual inspection of the sill seal, and keeping the drainage channel clear. One installer adds the sentence that matters most for a project of this size: improper drainage, incorrect sill levelling or inadequate fixing will cause problems regardless of product quality.
SL126 publishes two track heights: a high track at 43 mm and a low track at 8 mm. These are not the upper and lower limits of one dimension. They are two products, and the choice is made long before anyone talks about alloy.
| Seen from | 43 mm high track | 8 mm low track |
|---|---|---|
| What it buys | A retained water barrier at the threshold; the published bottom track water-blocking edge does more work | A step that most people do not notice and that a wheelchair, a trolley and a wet foot all do |
| What it costs | A visible upstand at the floor line, and an accessible-design conversation | Much less retained capacity, so the external drainage and the eave detail have to be right |
| Who argues about it | The accessibility reviewer and the person moving furniture | The person who owns the floor build-up and the external drain |
| Confirm before ordering | Finished floor level inside, and whether the door sits on an accessible route | Finished level outside, fall across the threshold, and where the water goes next |
The published drainage features attach to this choice rather than replacing it: a patented eave-style waterproof design and a bottom track water-blocking edge on the (96), a butyl gasket at the frame-sash joints and interchangeable drip-eave inserts on the (75).
The interchangeable drip-eave insert is worth singling out. It is one of very few published features anywhere in this catalogue that is explicitly about replacing a part in place, without replacing the profile. Ask what else on this door is replaceable in kind, and which of those parts have to be ordered in the original container rather than shipped later.
The finish is a separate specification. 6060 is a substrate designation and says nothing about the coating. Public comparisons of 6060 and 6063 put the difference plainly: 6060 has a finer microstructure and produces a more even anodic layer, which is why it is preferred where anodising is specified; for powder coating the difference is largely irrelevant, because the coating covers the microstructure entirely. Either way, temper and finish are two lines on an order, not one.
The corrosion and shear figures in this catalogue belong to one series. A 240 hour salt spray result and a 5000 N shear result are published for AW90 only. They do not transfer to SL126, they are not air permeability, water tightness or wind resistance classes, and no series in this catalogue publishes those classes at all. If your submittal requires them, they have to be requested as calculated or tested values for your configuration.
The alloy's own datasheet does not rate it for the coast. On the corrosion scale printed in the EN AW-6060 datasheet, general atmospheric corrosion is rated 1 and marine exposure is rated 2. The alloy is not the answer to a marine site; the coating specification, the fastener material and the maintenance regime are.
| Item | Published for SL126 | What you still have to ask for | Why the gap exists |
|---|---|---|---|
| Alloy and temper | 6060-T66 | Mill certificate with heat number and tensile results from the delivered batch; state EN 10204 3.1 or 3.2 in the order | Printed on every series in the catalogue, so it is a floor rather than a differentiator |
| Profile thickness | 2.0 mm, locally to 3.0 mm | A dimensioned section with the reinforced zones marked | "Critical areas" is a category, not a location |
| Thermal break material | PA66GF25, multi-chamber | Strip width in millimetres, and a frame calculation if you need a number | The material is published; the dimension that drives performance is not |
| Glass sash thickness | 55 mm | The glazing rebate dimension on the section drawing | 55 mm is the sash build-up, not the glass it will accept |
| Maximum single sash | 2.5 m by 3.0 m, about 7 square metres | The glass build-up that maximum was calculated against | The maximum moves when the glass gets heavier, and the baseline glass is not named |
| Rated sash capacity | not published | Kilograms per sash, for your glass configuration | In a lift-and-slide, this rating is what produces the seal compression |
| Corner construction | not described | Bracket and adhesive, crimped, or welded — and the section that shows it | Welding changes the temper in the most loaded zone, as the alloy datasheet states |
| Track height | 43 mm high, 8 mm low | Which one you are buying, plus finished floor levels inside and out | It is a choice, not a range |
| Thermal transmittance | not published for the sliding series | A calculated value for your size, mullion layout and glass | Sliding systems keep a running clearance; the published K values in this catalogue belong to the casement and tilt-turn families and are system values, not values for your opening |
| Air, water and wind classes | not published for any series | What your project requires, and who signs for it | A defect is a departure from a declared threshold. With no declared class, "the door leaks" is an argument rather than a measurement |
| Line | What to write | The answer that sounds right and says nothing |
|---|---|---|
| 1 | Full model code with suffix, track count and panel count | "SL126 series" |
| 2 | Opening method: sliding or lift-sliding, in writing | "Both are available" |
| 3 | Overall frame size in millimetres, width before height, as measured on site | "Standard size" |
| 4 | Exact glass build-up, including spacer and gas fill | "Standard double glazing" |
| 5 | Estimated sash weight, and the rated capacity of rollers and lift gear per sash | "It is heavy duty" |
| 6 | Thermal break strip width in millimetres and material certificate | "PA66 nylon" |
| 7 | Corner construction: bracket and adhesive, crimped, or welded | "Seamless corners" |
| 8 | Mill certificate type, heat number, and tensile results from the delivered batch | "6060-T66 aluminum" |
| 9 | Track height, 43 or 8, plus finished floor levels inside and out | "The installer will handle it" |
| 10 | Which replaceable parts ship with the original order | "Spare parts are always available" |
On the published minimum values, yes: 215 MPa tensile and 160 MPa yield against 160 MPa and 120 MPa for EN AW-6060-T5 in the same wall thickness band, with 6063-T5 quoted in public comparisons somewhere around 175 MPa tensile and 130 MPa yield, depending on the source. But the more useful reading is that T66 is a raised floor achieved by press quenching and process control, not a different metal. Two public sources give slightly different figures for the same temper, so treat the direction as reliable and the exact numbers as source-specific.
Not meaningfully. Hardness testing is a screening tool; the standard's validation is tensile. What you can check is documentation: a mill certificate with the heat number matching the packing, actual tensile results from the batch supplied, and a stated EN 10204 certificate type written into the order before production. If you want physical verification, agree the sampling procedure and the laboratory in advance.
We will not answer that for your project. Public summaries of GB/T 8478-2020 disagree on the minimum for an exterior door, quoting both 2.0 mm and 2.2 mm. Confirm the version your project adopts with the authority having jurisdiction and write it into the order. What we will say is that the same clause requires the wall thickness to be determined by design calculation and testing — which is why the location of the 3.0 mm reinforcement matters more than the nominal.
The published maximum sash for SL126 is 2.5 m by 3.0 m. Public thresholds from installers put the point where a lift mechanism becomes necessary at roughly 2.4 m of sash height, or at sash weights above about 200 kg. A 7 square metre panel with a conventional insulating unit is already in that territory on glass weight alone. Decide it in writing, and ask for the rated capacity.
43 mm if water retention at the threshold is the priority and an upstand is acceptable; 8 mm if step-free passage is the priority and the external drainage and eave detail are properly designed. They are separate products, not a range, and the finished floor levels on both sides have to be settled before manufacture.
Sliding systems must retain a running clearance so the sash can move, which means the sealing interface is fundamentally different from a compression-sealed casement. The published K values in this catalogue belong to the casement and tilt-turn families and are system values rather than values for a specific opening. Ask for a calculated value for your size, mullion layout and glass.